Factory lighting is a critical element for ensuring workplace safety, increasing production efficiency and saving energy in industrial facilities. Properly planned factory lighting systems raise employee performance, lower error rates and minimize operating costs.
The Importance of Factory Lighting
In production facilities with large areas and high ceilings, factory lighting is decisive for visibility and safety. Insufficient lighting can cause workplace accidents, eye strain and production errors. For this reason, the right light level and uniform distribution are very important in industrial lighting projects.
Ideal Factory Lighting Solutions for Industrial Facilities
LED Factory Lighting
LED factory lighting is the most preferred solution, thanks to its high energy efficiency and long life.
High-ceiling LED High Bay luminaires
deliver powerful light while lowering electricity consumption.
High-Ceiling Factory Lighting
Industrial luminaires used in high-ceiling areas ensure that light reaches the floor evenly. This creates a shadow-free, comfortable working environment in production areas.
Zone and Accent Lighting
At machine fronts, assembly lines and checkpoints, track spotlights and downlights increase visual precision. This strengthens the contribution of factory lighting to workplace safety.
Energy-Efficient Factory Lighting Systems
Thanks to LED technology, factory lighting solutions:
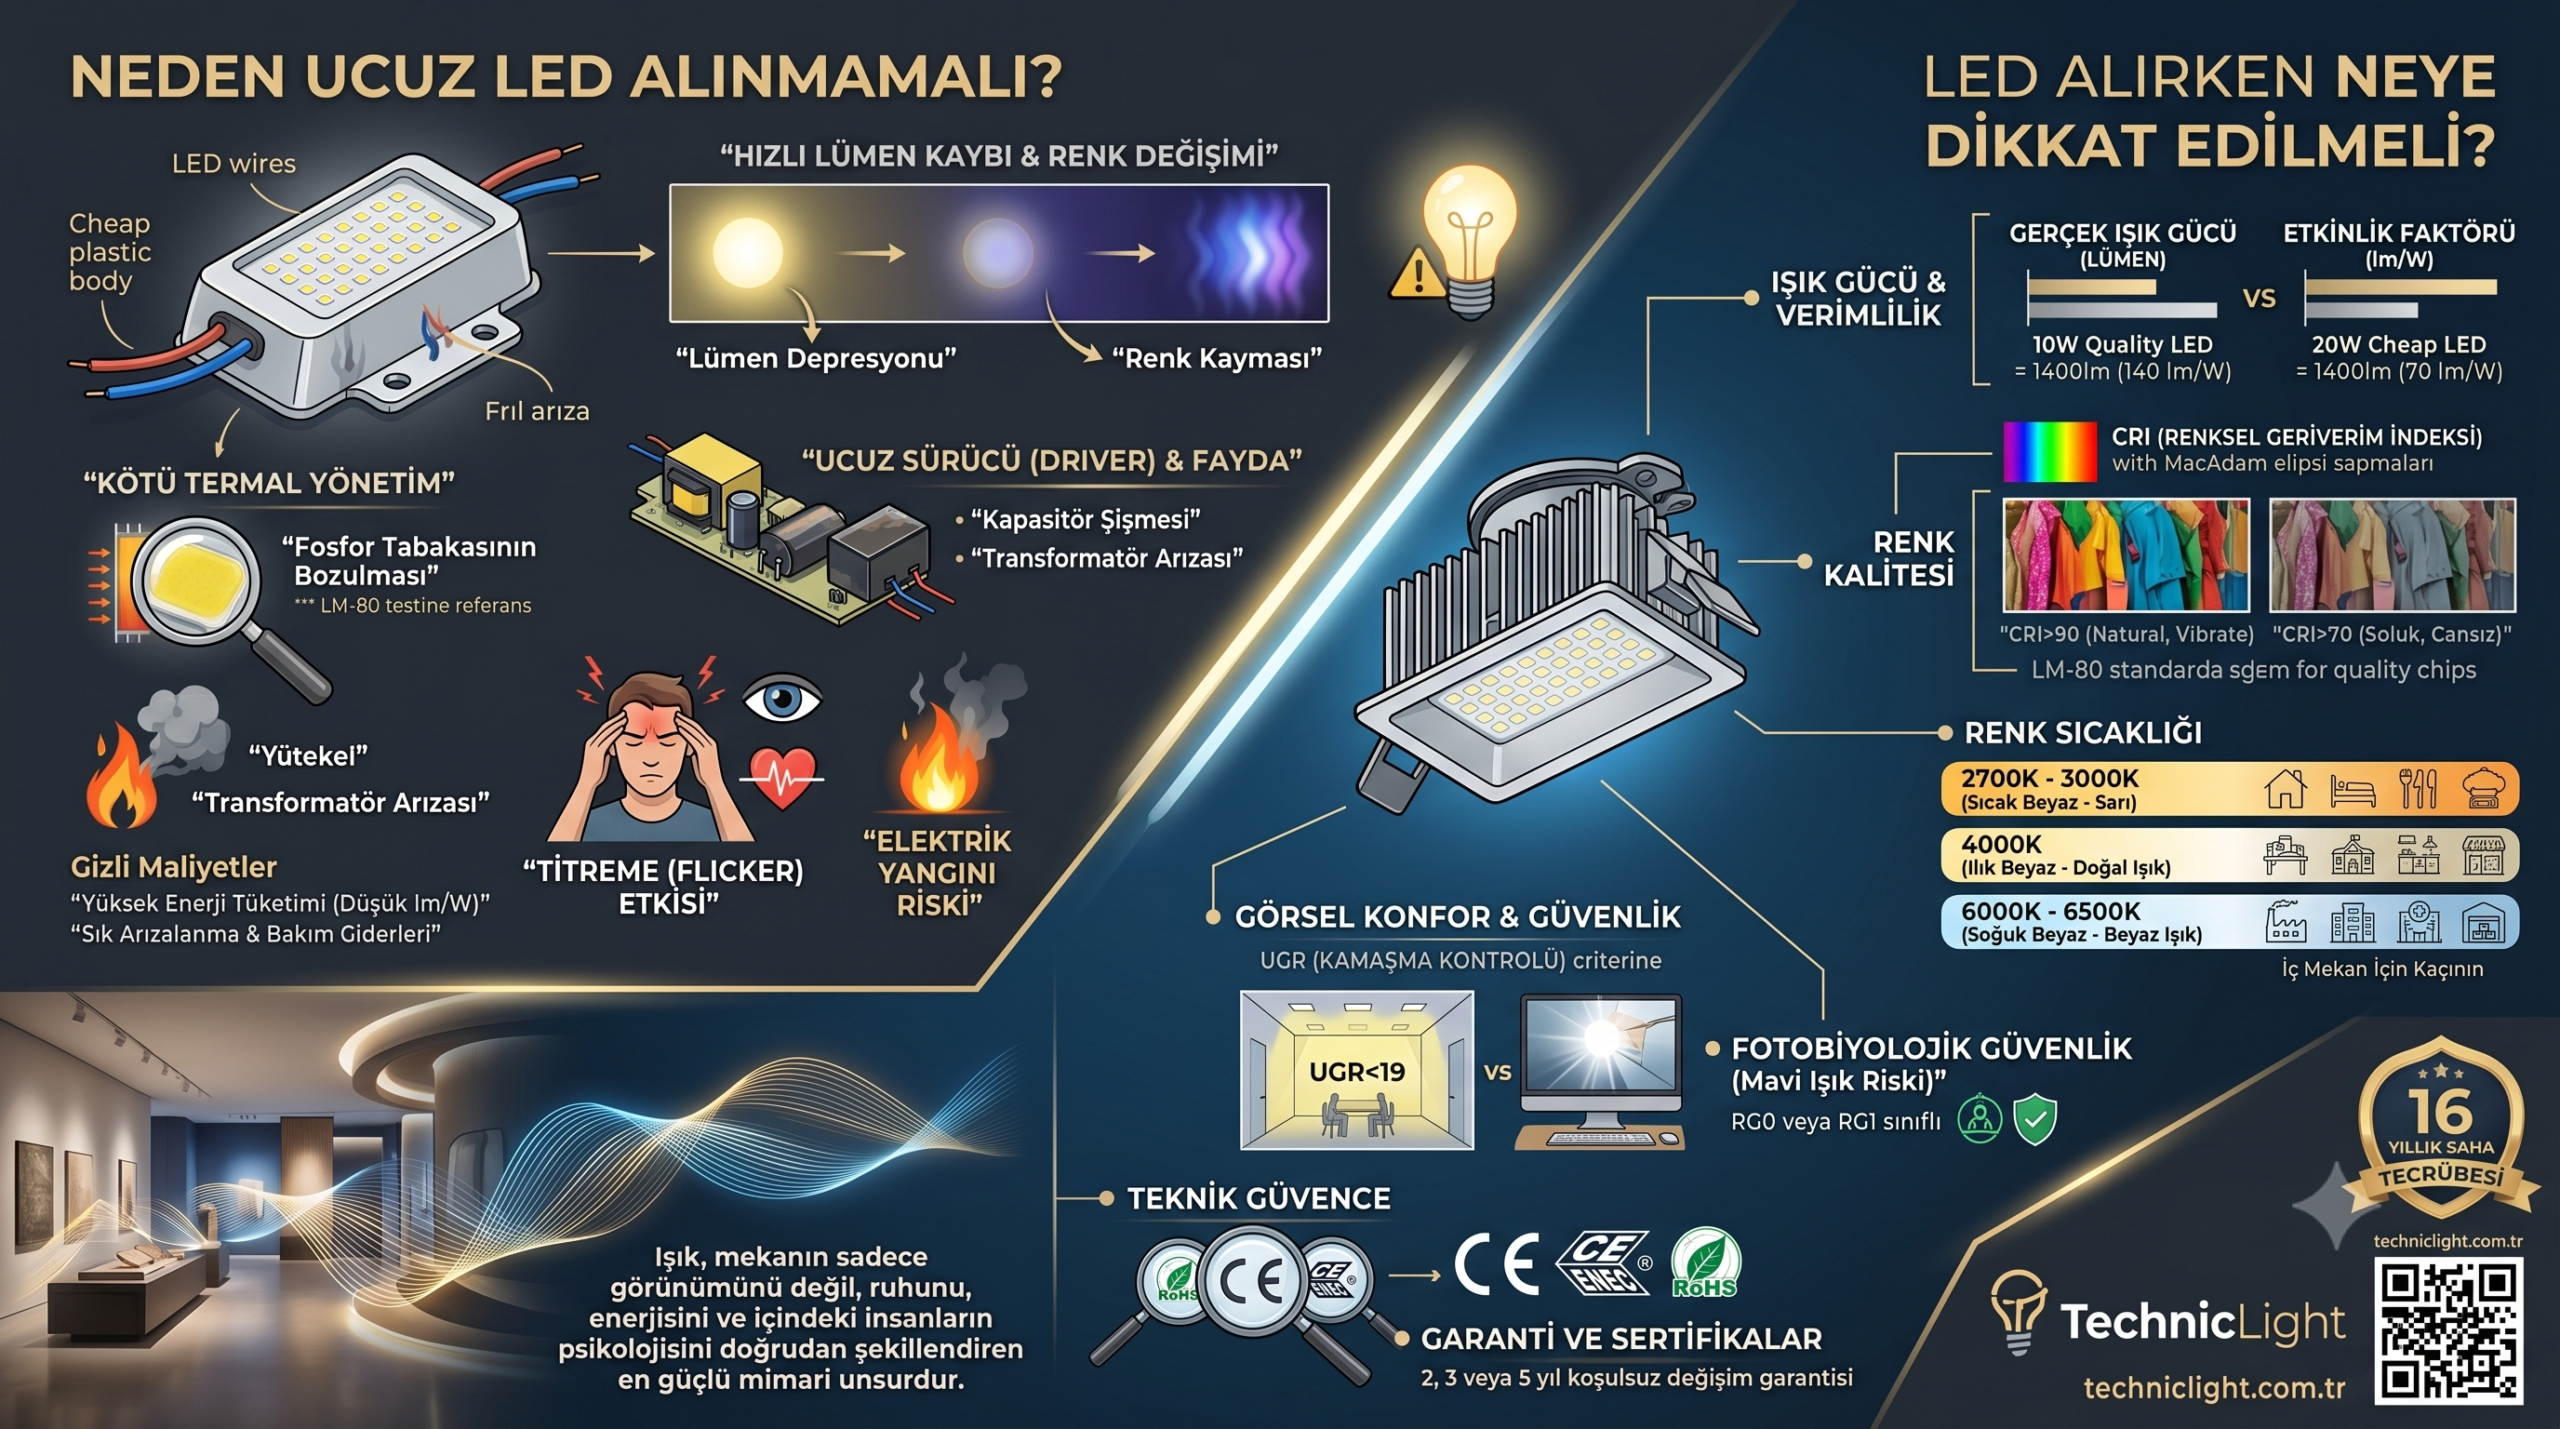
Save up to 60% energy
Have a long service life
Have low maintenance costs
Are environmentally friendly
offer these advantages.
What to Consider When Choosing Factory Lighting
Light level (lux): Must suit each production area
Color temperature: 4000K–6500K in production areas
Durability: IP-rated, industrial-grade luminaires
Ease of installation: Surface-mounted and modular systems
Conclusion
Properly planned factory lighting increases production quality, reduces workplace accidents and lowers energy costs. With LED-based industrial lighting solutions, you can build a system that is both sustainable and economical.
At TechnicLight, we offer the most efficient factory lighting solutions for your plant with surface-mounted LED luminaires, recessed LED luminaires, high-ceiling luminaires and track spotlight systems.